The standard concrete polishing grit sequence is 50 → 100 → 200 (metal or hybrid), then 400 → 800 → 1500 → 3000 (resin pads). You should not skip grits: each step removes the scratches of the previous one. Stop at 400 for satin, 800 for polished, and run to 1500-3000 plus burnishing for a mirror finish.
| Grit | Type | Effect |
|---|---|---|
| 30/60 | Metal bond | Flatten, open surface |
| 120/200 | Metal or hybrid | Remove coarse scratches |
| 400 | Resin | Satin sheen |
| 800 | Resin | Polished look |
| 1500 | Resin | Clear reflection |
| 3000 | Resin | High-gloss mirror |
A 3000-grit pad is too fine to cut a 400-grit scratch. If you jump from 400 to 1500, the 400 scratches remain trapped under a glossy surface — you see them as a haze. Each grit must fully remove the previous pattern before moving up. Inspect by raking light between steps.
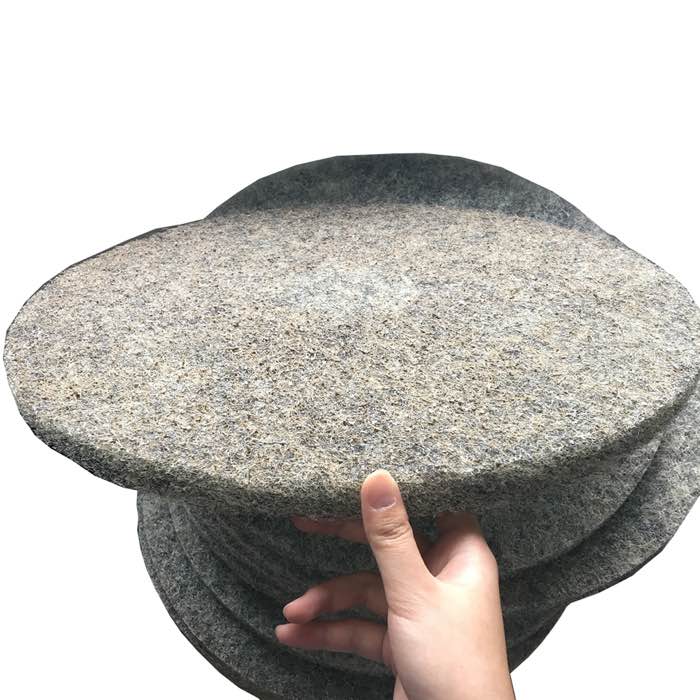
The hardest jump is from 200 metal to 400 resin. Many pros add a hybrid copper-bond or ceramic transitional pad such as the copper-bond transitional pads or ceramic-bond transitional pads to wipe out metal scratches before the resin stage.
Many contractors run metal and early resin grits dry with vacuum, then switch to wet polishing for 800 and above to get clarity. Others go fully dry. Wet gives deeper gloss on hard concrete; dry is cleaner and faster. Test both on a sample patch.
Coarse pads (50-200) wear fastest, covering tens of square meters. Fine pads (1500-3000) last longest because they cut gently. Budget more pads for the early steps and fewer for the final gloss. Replace pads when they load or glaze — a worn pad cannot remove the previous scratch.
If you follow the grit sequence and still get haze, the cause is usually skipped densifier, a soft weak cream, or residual laitance. Back up, densify properly, and re-run. Grit alone cannot build a shine on unhardened concrete.
Stop at each grit, rinse or vacuum, and inspect at a low angle. If you see the previous grit's scratches, keep grinding — do not move up. This discipline is what separates a professional shine from a dull haze.
Store resin pads flat and dry. Heat warps them. Keep grit sets together so you do not lose numbers. Label bags by grit. A mixed-up set causes skipped-grit mistakes on the job.
Replace a pad when it stops removing the previous scratch, even if it looks intact. Worn pads waste time. Keep a few spares of each grit on the truck.
After 1500 or 3000, run a dry wool or resin burnishing pad at high speed. This is the step that turns a good polish into a reflection. Skip it and the floor looks flat rather than glossy.
Start at 50 or 100 metal. Step 200, then transition. Resin 400, 800, 1500, 3000. Densify between. Burnish at the end. Do not skip grits. Vacuum between steps. Stop at the sheen you planned. This sequence is proven on millions of square meters.
Coarse pads wear fastest; fine pads last longest. Budget replacements for the early steps. A worn pad wastes more time than it saves.
The grit sequence is a ladder — skip a rung and you fall. Run each step fully, use transition pads, stop at the sheen you need.
Inspect at every grit with raking light. It takes minutes and prevents a finished floor that looks wrong from ten feet away.
Label your pad bags by grit. Mixing them up on site is a common and costly mistake.
A final high-speed burnish turns a good polish into a reflection.
A consistent sequence beats any shortcut. Stick to the grit ladder and the floor will shine.
A: No. Skipping leaves 400-grit micro-scratches that reduce clarity.
2-3 overlapping passes until the floor is uniformly textured at that grit.
Only for a mirror showroom finish. Most commercial floors stop at 800-1500.
Mostly, but resin pad branding varies; follow the printed number on the pad.
The grit sequence is a ladder — skip a rung and you fall. Run each step fully, use transition pads, and stop at the sheen you need. Contact JOY TECH for a full 50-3000 resin pad set matched to your grinder.