Removing a thin acrylic sealer from concrete usually takes 1–2 grinding passes with metal-bond tooling at 30/40 grit. Acrylic sealers are thin (0.1–0.3mm) and grind away quickly, but they tend to gum up segments if the machine runs hot. The reliable sequence is: one pass to break the sealer film, vacuum and inspect, then a second pass to clean the remaining sheen and open the concrete to CSP 1–2. Thicker coatings (epoxy, urethane, or multiple sealer layers) need PCD tooling first and 2–4 passes total.
If you can feel the coating with a fingernail and it scrapes off in flakes, it’s light. If it resists scraping or is thicker than 0.5mm, treat it as a medium coating and start with PCD.
| Coating | Tooling | Passes | Profile Result |
|---|---|---|---|
| Acrylic sealer (single coat) | 30/40 metal bond | 1–2 | CSP 1–2 |
| Acrylic sealer (multiple coats) | 30/40 metal bond | 2–3 | CSP 2 |
| Thin epoxy / urethane (under 0.5mm) | PCD then 30/40 | 2–4 | CSP 2–3 |
| Failed penetrant sheen only | 80/100 metal bond | 1 | CSP 1 |
A: Yes, for small areas. Use a 5''/125mm cup wheel at 30/40 grit with a dust shroud. It takes 2–3 minutes per square meter, versus 30–60 seconds with a walk-behind grinder.
A: Acrylic melts under heat and friction, coating the diamonds. Reduce pressure, increase travel speed, let the disc cool between passes, or switch to PCD tooling which shears rather than grinds.
A> 30/40 grit metal-bond cuts the fastest while leaving a CSP 1–2 profile. Finer grits polish instead of remove and can smear the sealer across the floor.
A: Usually yes. Chemical strippers soften the sealer but leave residue and surface contamination. A single 30/40 pass cleans the floor and restores a proper profile.
A> The surface should look uniformly gray with no glossy patches. Mist water on a small area — it should soak in quickly rather than bead up. If it beads, more passes are needed.
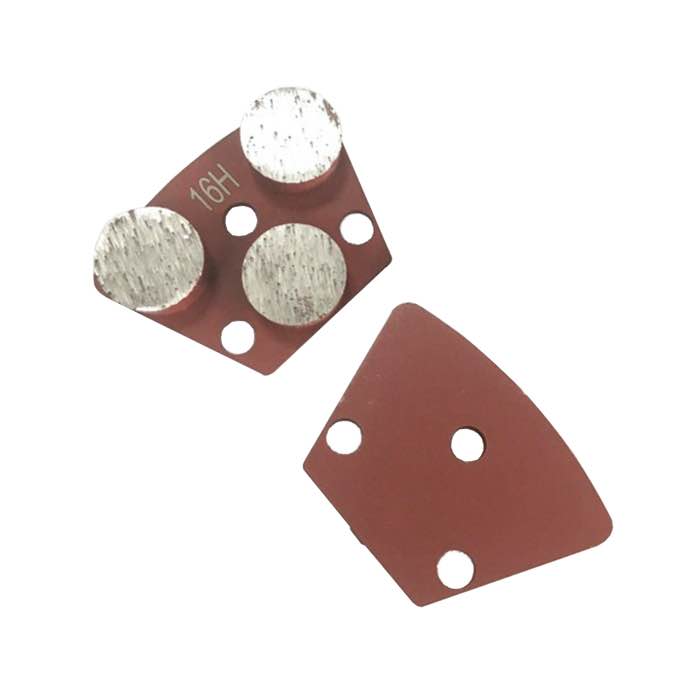
Light acrylic sealers need just 1–2 grinding passes at 30/40 grit, run with light pressure and continuous dust control. Inspect between passes, let hot segments cool, and switch to PCD for anything thicker. JOY TECH offers 30/40 metal-bond discs and PCD tooling for every coating scenario.