Laser-Welded vs Vacuum-Brazed Core Bits for Brick and Block
Laser-Welded vs Vacuum-Brazed Core Bits for Brick and Block
Quick Answer
Use a laser-welded core bit for abrasive brick, block and hard masonry where segment bond strength and long life matter. Use a vacuum-brazed core bit for clean, fast cutting in softer brick, tile and thin masonry where a single layer of diamond on a steel body gives the lowest cost per hole. Laser welding is for impact and abrasion; vacuum brazing is for speed and light duty.
How the Two Bonds Differ
A laser-welded bit has a sintered diamond segment welded to the steel barrel. The segment contains diamond throughout its depth, so as it wears, fresh diamond is exposed. The weld is a structural joint that tolerates heat and impact.
A vacuum-brazed bit has a single layer of diamond brazed onto the steel rim. It cuts fast because the diamond is exposed, but once the layer wears through, the bit is finished. There is no segment to dress or re-sharpen.
Cutting Speed and Life
Vacuum-brazed bits cut faster in soft brick and block because the exposed diamond has a aggressive edge and the bit has a thin kerf. In hard engineering brick or concrete block, the single layer wears quickly and the bit may fail after a few holes.
Laser-welded bits start slower but hold their diameter and cut rate for many more holes. In abrasive masonry, the segment wears evenly and the bit can be used until the segment height is exhausted.
| Material | Better choice | Why |
|---|---|---|
| Soft clay brick | Vacuum-brazed | Fast, low cost per hole |
| Engineering brick | Laser-welded | Abrasion resistance |
| Concrete block | Laser-welded | Holds diameter in aggregate |
| Tile and thin masonry | Vacuum-brazed | Clean, fast entry |
When Laser Welding Is Worth the Price
Laser-welded bits cost more, but the cost per hole can be lower when the bit lasts 5-10 times longer. On a production site drilling hundreds of holes in block, the labour cost of changing bits and the risk of a stalled hole outweigh the unit price. Laser welding also tolerates the heat of dry drilling better than a brazed single layer.
For a contractor drilling a few holes in soft brick, the vacuum-brazed bit is the better economic choice. For a distributor stocking one bit that must handle unknown masonry, laser-welded is the safer specification.
Water and Dust
Both types can be used wet or dry, but water management differs. A vacuum-brazed bit in soft brick can be run dry with a dust extractor; a laser-welded bit in concrete block should be run wet or with a high-capacity shroud to control heat. Never run a dry bit at high pressure without clearing dust; the kerf will pack and the bit will bind.
Frequently Asked Questions
Q: Can a vacuum-brazed bit drill concrete?
A: It can drill light concrete and tile, but it wears fast in abrasive aggregate. For repeated concrete holes, use a laser-welded or sintered segment bit.
Q: Why is my laser-welded bit slower at the start?
A: The segment has a wider contact area and needs a short break-in. Let the bit cut its own seat and do not force it.
Q: Which bit leaves a cleaner hole in brick?
A: A vacuum-brazed bit usually leaves a cleaner entry in soft brick; a laser-welded bit can chip more at the start until the segment seats.
Q: Can I resharpen a vacuum-brazed bit?
A: No. Once the single diamond layer is worn through, the bit is spent. Replace it.
Conclusion
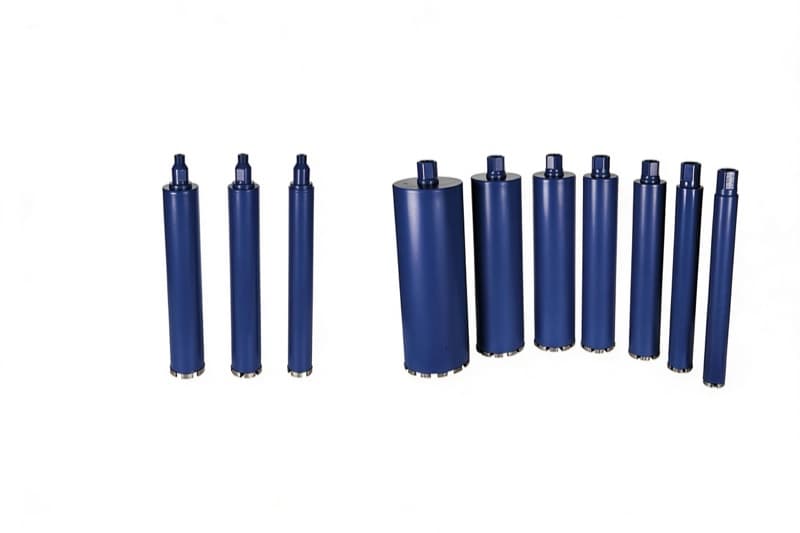
Choose vacuum-brazed for speed and low cost in soft brick and tile; choose laser-welded for abrasive block, hard brick and repeated production holes. JOY TECH supplies laser-welded wet core bits and a full range of diamond core drill bits for masonry and concrete.
Products used in this guide
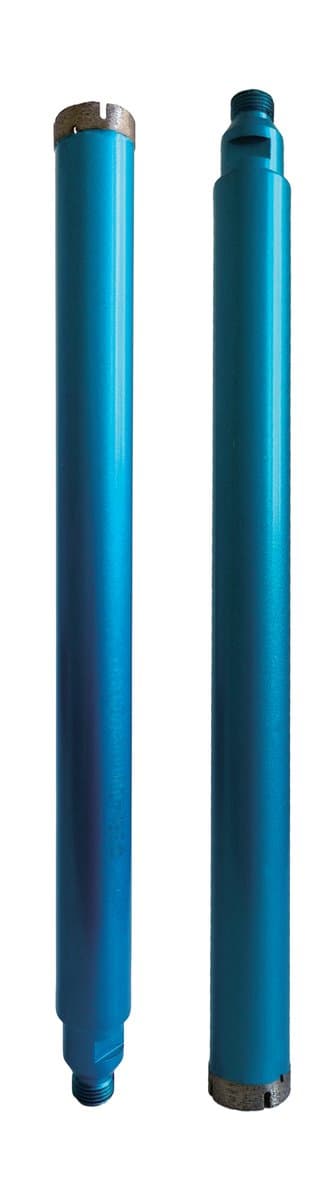
Laser Welded Thin-Wall Core Drill Bit — LWC Series
View specs →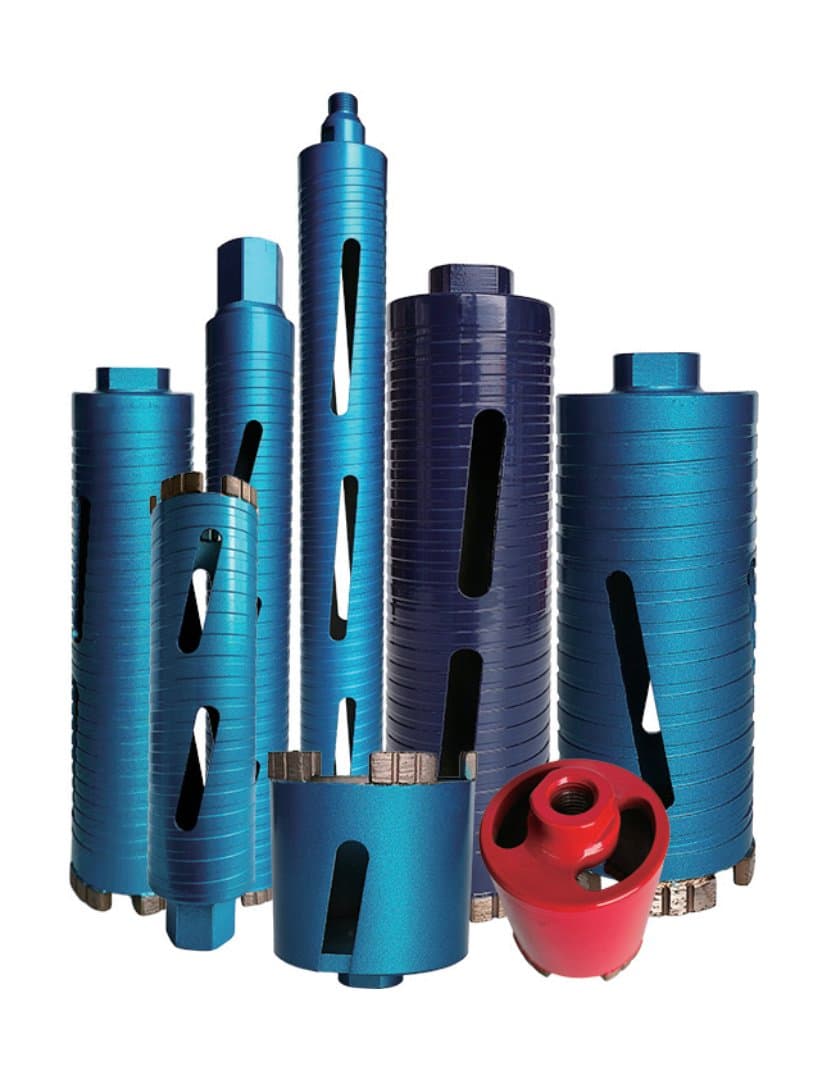
Laser Welded Dry Core Drill Bit — LD Series
View specs →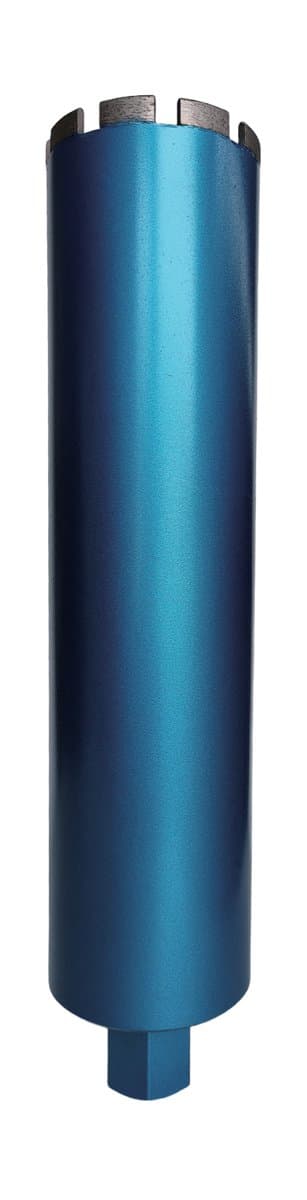
Laser Welded Wet Core Drill Bit — LWR Series
View specs →Need this tool for your job?
MOQ 1 · 7–30 days by order quantity · FOB & CIF · free sample on request
Author & Manufacturer
Written and reviewed by JOY TECH — an SGS & BV audited, CE/RoHS certified diamond tools manufacturer founded in 2004, exporting to 50+ countries.
Quality & Compliance
Our factory and QMS are audited by SGS and Bureau Veritas. Products meet CE/RoHS requirements and every piece is 100% inspected before packing.
Verified Certificates
- SGS Audited Supplier — Report No. QIP-ASI227442 & QIP-ASR247051 (Audit Jan 29, 2024)
- Bureau Veritas Verified — Report No. MIC-ASR257059 (Audit Feb 20, 2025)
- CE & RoHS Certificate of Conformity — No. CS240925001HRZ (Issue Sep 25, 2024)