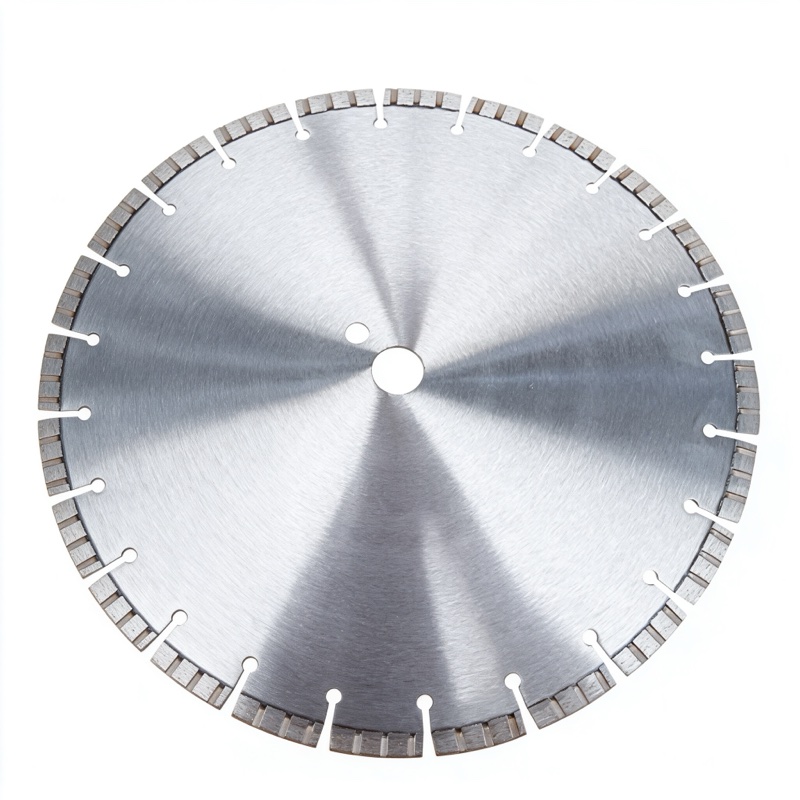
A blade that spins but stops cutting is usually glazed (dulled) or the wrong bond for the material. Check the direction of rotation, RPM, and the segment face first — then dress the blade on an abrasive block or switch to a softer bond.
| Symptom | Cause | Fix |
|---|---|---|
| Shiny segments, no cut | Glazed / bond too hard | Dress on abrasive block |
| Spins but no progress | Backwards rotation | Check arrow direction |
| Overheating, slow cut | Wrong RPM or dry cut | Adjust speed / add water |
| Cut slows over time | Wrong bond for material | Switch bond hardness |
A: When the cut slows and the segments look shiny. Regular light dressing keeps the cut fast.
A: Most glazed blades recover with dressing. Only replace a blade that is cracked, warped, or has lost segments.
A: Water helps cooling, but glazing needs mechanical dressing to expose fresh diamond.
Check rotation and RPM first, then dress the blade. If glazing keeps coming back, the bond is wrong for the job — for tough concrete work, try the Concrete and Asphalt Saw Blade (Laser Welded) — JOY-CA-LW; for granite, the Granite Saw Blade (Long Segment) — JOY-GR-L.